Industry
Point cloud, isometric, folding rule: Why manual measurement remains indispensable
The isometric comes from the laser scan, yet the supervisor still double-checks the pump nozzle on site. Where those millimetres come from, why manual field measurement remains a craft for stress-free installation — and why the real risk is the sheet of paper the dimensions end up on afterwards.
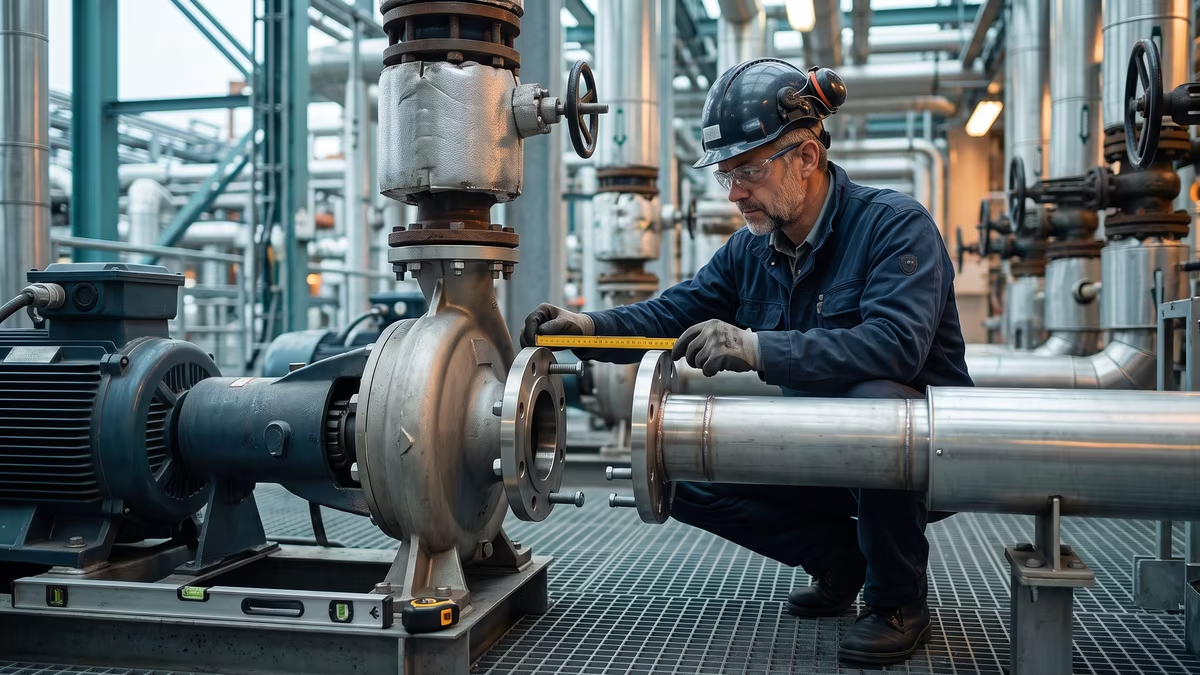 AI-generated
A typical turnaround scenario: The isometric for the new pressure line at the pump is in the workshop, Revision B, modeled from a laser scan. The tie-in spool is scheduled for fabrication tomorrow. “The iso came from the point cloud, it fits,” says the work prep engineer. The foreman still grabs a tape measure, spirit level, and string line and heads to the pressure nozzle. “Better to measure now than fetch the chain hoist later.” Half an hour later, there is a sketch on the back of the iso — with a centerline dimension that differs from the drawing by twelve millimeters.
Twelve millimeters is too much for a gasket and too little for a complete redesign.
A pipeline designed from a point cloud does not automatically fit stress-free, because every stage from the scan to the installed spool introduces its own deviations — measurement, registration, modeling, fabrication, installation — and they all accumulate at the tie-in point. That is why, based on field experience, isos generated from point clouds rarely fit accurately enough at existing equipment, pumps, or vessels to allow blind prefabrication and stress-free installation.
This article explains where those millimeters come from, why manual verification is part of the job — and why the real problem only begins once the dimension is written down.
Many small millimeters become a tolerance stack-up at the nozzle
First, to be fair: Without laser scanning, some brownfield design work would hardly be possible. But the point cloud remains a measurement result. Several links are involved before the spool is installed:
- The scanner measures points, not flanges. Datasheets typically specify around 2 millimeters point accuracy over 10 meters — for a single scan on a bright surface. Depending on resolution and distance, point spacing ranges from a few millimeters to more than a centimeter; only a few points may hit a bolt hole. Gasket faces and nozzle centerlines are derived by fitting planes and cylinders. A one-millimeter error over a 200-millimeter gasket face equals roughly 0.3 degrees — about the same angular misalignment ASME PCC-1 allows for a flange pair before tightening.
- Registration combines many scans — and can accumulate errors. The small registration error mainly indicates how well adjacent scans fit together, not how accurately the overall model is positioned. DVW Bulletin 18-2022 describes a tolerance verification on an industrial construction site with 370 scans: after adjustment, the registrations differed from each other by an average of 0.2 millimeters, but by an average of 3.3 and a maximum of 7.7 millimeters compared to tachymetrically surveyed tie-in points.
- The scan captures the day of recording, not the day of installation. If scanning is done during operation and installation during shutdown, a hot line will no longer be where it was scanned. For comparison: 10 meters of carbon steel changes length by roughly 18 millimeters with a temperature difference of 150 Kelvin. How much of that movement reaches the nozzle depends on anchors and guides.
- The workshop and weld seam add their share. EN 13480-4 defines tolerance classes for prefabricated spools, with permissible deviations ranging from one to several millimeters. In addition, every butt weld shrinks, typically by one to three millimeters depending on wall thickness and weld preparation, and even more on heavy-wall pipe. The most reliable values come from your own fabrication experience.
Not every link deviates in the same direction. But at an individual flange, it only takes two unfavorable ones to coincide.
Stress-free means: the flange fits before the first bolt is tightened
EN 13480-4 does not permit pipelines to be forced into alignment for a connection — unless preload is explicitly specified in the design. Flanges must be brought together flat and square without force. Depending on nominal size, the VCI flange assembly guideline allows a flange gap of 0.4 to 1.0 millimeters — and explicitly states: if the flange position can only be achieved using a chain hoist or come-along, the gap is unacceptable.
More stringent standards apply at pumps than at ordinary flange pairs: pump manufacturers prohibit using the pump as a fixed point for the pipeline, and PCC-1 refers to API RP 686. Verification is done with a dial indicator at the coupling: if the shaft moves while the flange bolts are tightened, the pipeline is imposing stress. The coupling is therefore checked again after pipe connection.
What a flange pair can tolerate is therefore less than the tolerance stack-up can produce. Blind prefabrication from the iso followed by stress-free installation is therefore rarely successful at tie-ins — not because of statistics, but because of field reality. Good engineering provides an overlength field weld for this reason; project conventions commonly allow an extra 100 to 150 millimeters. If that allowance is missing or insufficient, the site measurement decides.
Tape measure, spirit level, plumb bob: manual field measurement is not failure, but craftsmanship
That is why the plant contractor goes to the tie-in point before the workshop starts cutting: tape measure and measuring tape, spirit level and angle finder, plumb bob and string line. Measurements are taken where the pipe will actually connect — ideally only after the pump has been aligned, the old line disconnected, supports installed, and spring hangers blocked. If measurements are taken weeks earlier during live operation, the field measurement suffers from the same condition-related issue as the scan. Then the isometric is sketched.
The tenths of a millimeter at the flange come from the sequence, not the tape measure: the line is supported before the pump, and the tie-in piece is installed last. The flange is positioned freely against the nozzle with a gasket or spacer matching gasket thickness and with centering bolts, the field weld is tack welded in that position, and only then fully welded. For verification, the bolts are loosened again: if the flange springs away, stress is present in the line.
The field measurement is where design and reality are reconciled — by someone who understands what is being measured.
The problem is not the measurement, but what happens to the dimensions afterward
What happens after the field measurement determines whether it is useful. A typical workflow has these weak points:
- The paper note. The sketch gets wet, smudged, ends up in a jacket pocket. The dimension exists in exactly one place.
- The phone photo. The sketch is sent via messenger to a private phone, with no reference to project, drawing number, or revision.
- The verbal instruction. “Make the tie-in piece 1,240.” Centerline dimension or cut length? The difference is enough to require a new tie-in piece.
- The manual data entry. In the workshop, 1,240 becomes 1,420 in the cut list. Measured correctly, transmitted incorrectly.
- The iso that is no longer correct. The isometric in engineering still shows the planned dimension. The next revision is based on the drawing, not the actual plant.
- The final documentation. Weld numbers and bill of materials refer to an iso that was never actually built that way. The additional field weld is missing.
In piping construction, this carries weight: during a shutdown, every hour counts, and for the next modification, the documentation becomes the planning basis again. Where VOB/B applies, the contractor must review supplied documents for inconsistencies insofar as required for proper execution and notify the client of discovered or suspected defects, submit concerns in writing and preferably before work begins, and announce an additional field weld as extra work before execution. The contractor must prove this independently — a dimension on a lost note proves nothing.
What pAIpe contributes: measure as always, manage as today
pAIpe replaces neither the tape measure nor the point cloud. It addresses the point where today the paper note takes over.
The fitter sketches the isometric on a tablet instead of paper. When opening a drawing from the work package as a template, the sketch inherits the drawing number and work package; the pipe class from the work package is preselected. Pipes are drawn with a finger, and the app inserts elbows automatically when direction changes. The measured overall dimension is entered per axis; the app subtracts the fitting face-to-face dimensions from the component database and calculates the pipe length between fittings — documented instead of shouted across the shop. Weld gap, shrinkage, and fit-up allowance are still defined by the workshop, and the face-to-face dimensions in the component database must match the supplied components.
With “Send to Platform,” the app checks the drawing for collisions and sends it into the project as a structured dataset. Sender and timestamp are recorded, and the drawing is available there for review; ideally, it is sent directly from site. Welds are automatically numbered, and a bill of materials is generated from the isometric. In the web interface, welders are assigned to welds and material batches are recorded. If documentation has been created for the work package, the isometric with weld and installation levels is incorporated there. It can also be exported as a DXF and returned to engineering — the comparison with the planned revision is still done by a person, but using the actual field measurement instead of a photo.
The measurement is taken the same way as always — and after sending, it remains permanently within the project.
If you would like to see how a field measurement moves from tablet to bill of materials and weld documentation, we would be happy to show you in a short conversation — demonstrated using an isometric from your day-to-day work.